Mechanical Distance
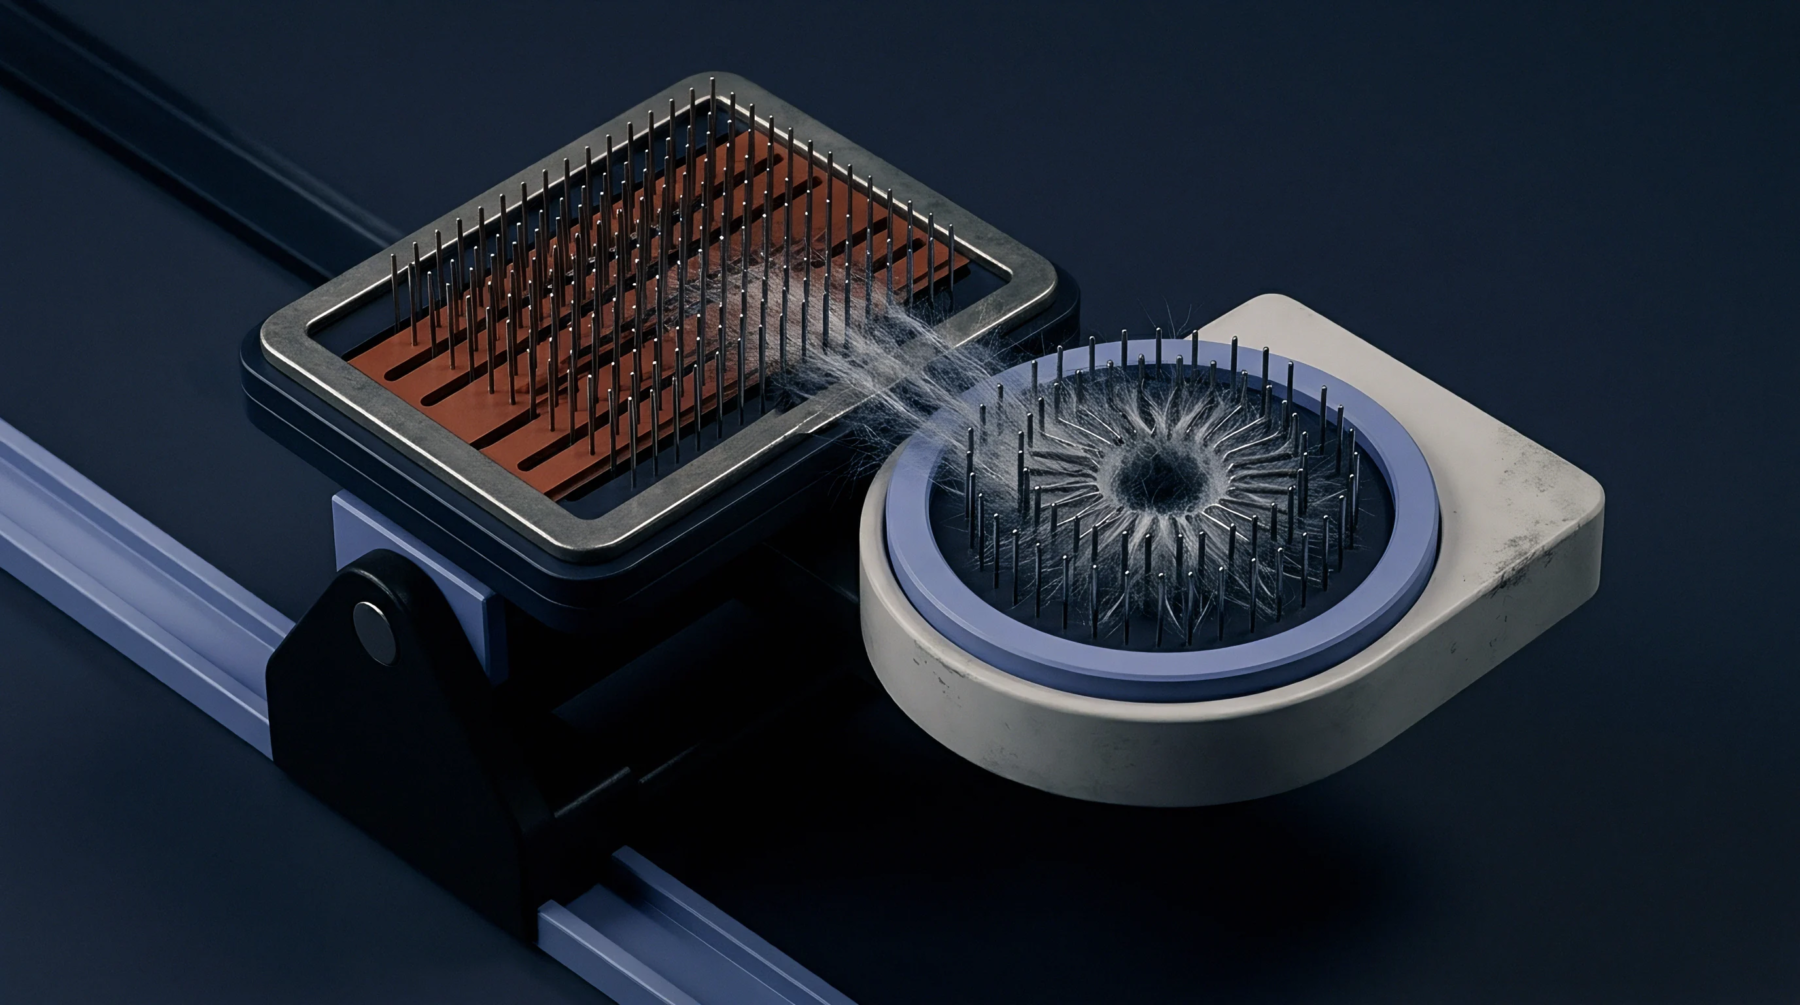
The narrow physical interval between the rotating carding cylinder and the stationary flats defines the carding clearance. Adjusting this spacing dictates the level of fibre separation and the removal of short fibres or trash particles during the opening process. Operators perform these adjustments to match the specific staple length of the cotton or synthetic stock.
Consistency across the full width of the machine ensures an even web formation, preventing uneven mass distribution that harms subsequent drawing or spinning stages.
Setting Protocol
Technicians calibrate these gaps using feeler gauges to maintain uniformity across the width of the machine. Frequent monitoring stops the accumulation of nep clusters that arise when the settings drift beyond tolerance. High speed processing creates thermal expansion in metal components, which shifts the real distance between surfaces during continuous operation.
Modern equipment utilizes automated sensors to compensate for this heat induced movement. Sensors maintain the desired geometry without manual intervention, protecting the clothing from potential damage caused by metal to metal contact.
Operational Consequence
Precision in these settings influences the waste percentage extracted at the cylinder. Tightening the gap increases the action on individual fibres, which improves cleaning but raises the risk of fibre rupture if the setting is too aggressive. Loose settings allow impurities to bypass the cleaning zone, which degrades the quality of the sliver and produces defects in the final yarn.
Correct alignment supports the parallelization of fibres, which reduces end breakages during high speed spinning.
Control Parameter
Establishing the correct value depends on the fibre fineness and the target quality of the yarn. Fine fibres demand tighter settings to ensure proper individualization without causing excessive stress to the material. Coarse fibres allow for wider settings, which reduces the load on the machine clothing and extends the maintenance interval.
Standardizing these values across a production line produces consistent sliver quality, ensuring that every batch meets the predefined strength and uniformity requirements. Correctly maintained clearance levels provide the foundation for stable production output.